Table of Contents
- What do you need to prepare before using a dunnage bag?
- The 5-step procedure for container dunnage bags (Kraft and woven PP)
- How to use carton void-fill air bags (light loads)
- Common mistakes when using dunnage bags
- Frequently asked questions about using dunnage bags
- Do I need a pressure gauge when inflating a dunnage bag?
- Can a Kraft paper dunnage bag be reused?
- How do I protect a dunnage bag from the sharp edges of a wooden pallet?
- Can a dunnage bag burst when the container sits in the hot sun?
- Can I use a bicycle or motorbike pump to inflate a dunnage bag?
- How much wider than the gap must the bag be?
- Can I put a dunnage bag at the container door?
- Contact us for technical advice and to buy dunnage bags
- References
Reviewed and updated by ICD - Week 44/2026
Using a dunnage bag takes five steps: put a protective board over sharp edges, place the bag in the middle of the gap, connect an inflation gun with a gauge, inflate to the pressure the manufacturer recommends (about 0.2 bar for a Level 1 paper bag), then close the valve and check again before closing the container door. The bag size must suit the gap: for example, an 80 x 120 cm paper bag is for a gap of up to 40 cm according to the ICD Vietnam specification table.
I am Le Van Thang, and I have worked in packaging supplies at ICD Vietnam since 2011. Most dunnage bag problems I am called in to look at are not about bag quality but about handling: a bag that does not suit the gap, pallet edges left unprotected, inflation by feel. This article gives a step-by-step guide for Kraft paper bags, woven PP bags and, separately, carton void-fill air bags, together with the CTU Code packing rules that many people skip.
What do you need to prepare before using a dunnage bag?
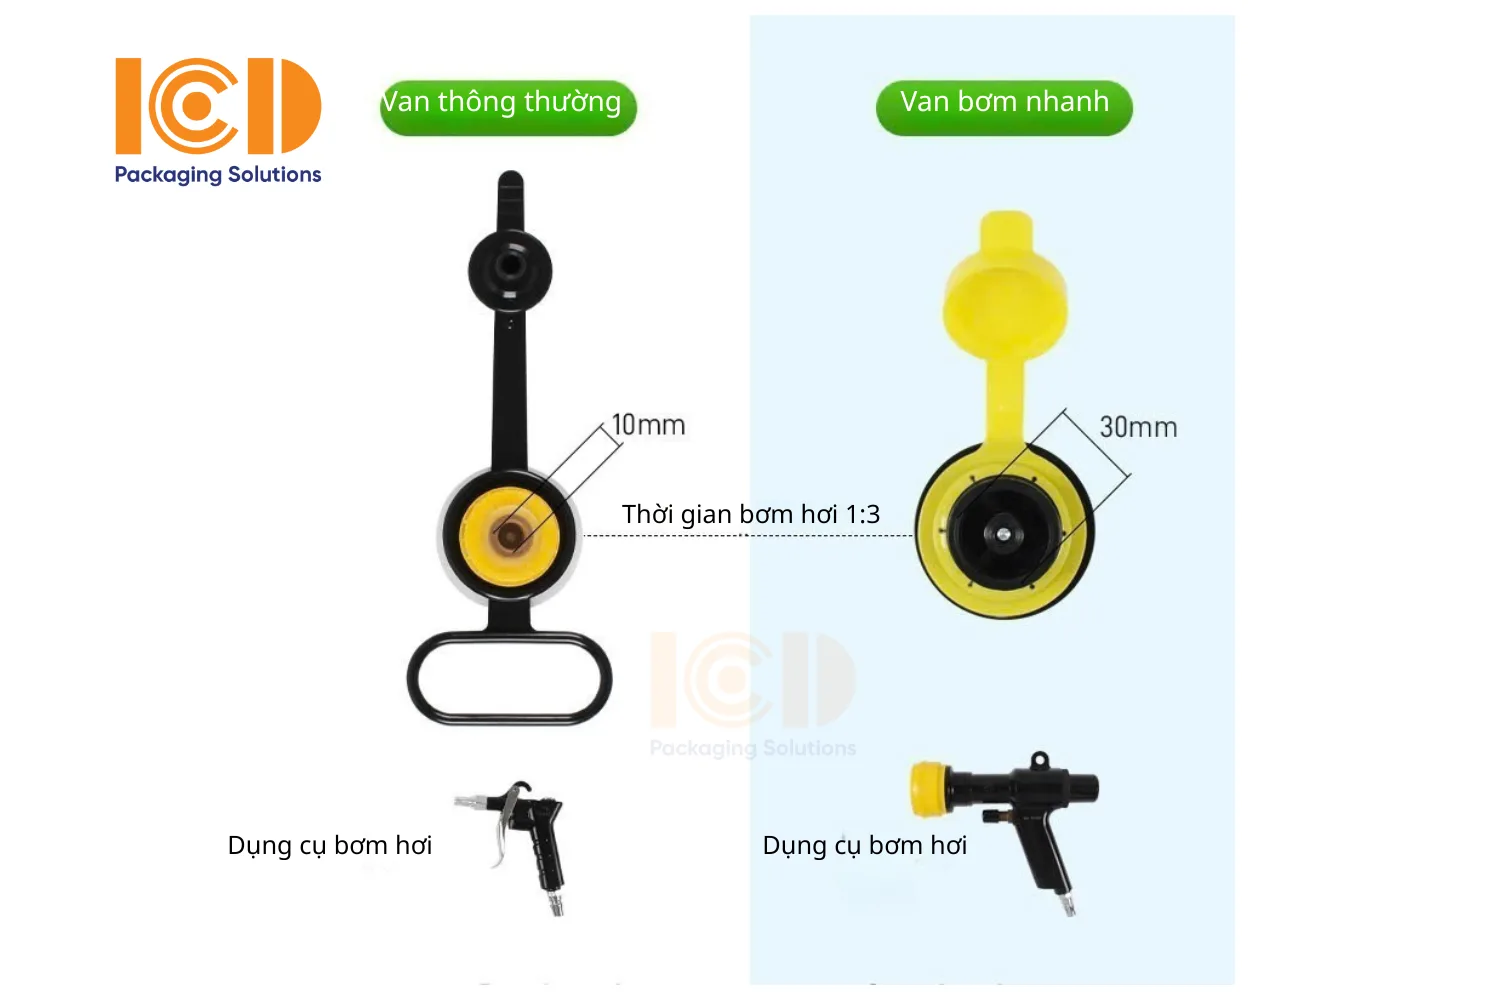
Before blocking the load, you need to know which bag type you are using, have an inflation device that fits the bag valve, measure the gap and have padding boards ready. Using the wrong inflation device is a common cause of leaks or under-inflation, especially in a warehouse that holds both small-valve bags and quick-fill valve bags.
Bag types and the matching inflation equipment
| Bag type | Main use | Inflation equipment |
|---|---|---|
| Kraft paper bag (Level 1 is the usual choice) | Cartons, palletised cargo, ordinary transport | Dedicated compressed-air gun matching the bag valve (standard or quick-fill valve), with a pressure gauge |
| Woven PP fabric bag (Level 0 to 5) | Heavy cargo, sharp edges, cargo where bags will be reused | Dedicated compressed-air gun with a gauge, matching the quick-fill valve |
| Carton void-fill air bag (PE/LLDPE) | Cushioning and filling small gaps inside a box | Small electric pump that makes the cushion on the spot; do not use industrial compressed air |
The levels in the table are taken from the ICD Vietnam catalogue. Paper and PP bags are not automatically “light” or “heavy”; the strength level is decided by the construction of each code, so when you receive bags, read the level label and the working pressure printed on the bag or on the specification sheet before inflating.
How big a gap suits a bag? (Max Void)
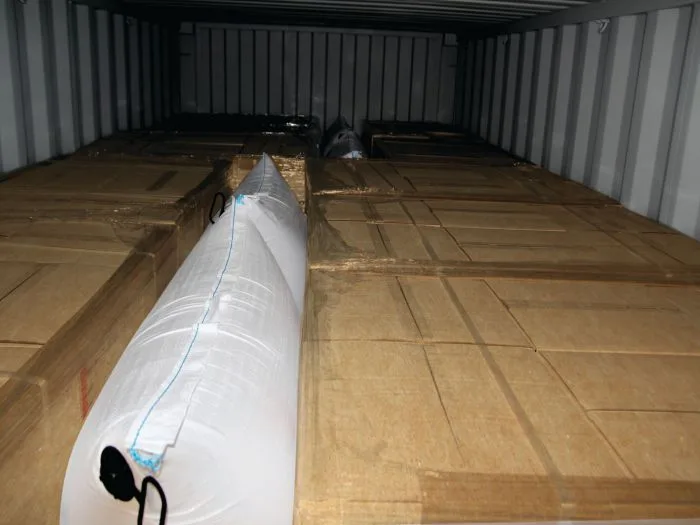
The maximum gap (Max Void) of each bag is set by the manufacturer according to the bag size, and the CTU Code requires following those instructions for inflation pressure and maximum gap. The reason is that when inflated the bag swells and shortens sideways, so the gap must not be wider than the bag can still press flat once inflated. The table below quotes some Kraft paper bag sizes from the ICD Vietnam product page.
| Flat bag size | Width after inflation | Maximum gap | Suggested use |
|---|---|---|---|
| 50 x 100 cm | 30 - 35 cm | 25 cm | Narrow gaps, small units, light cartons |
| 80 x 120 cm | 50 - 55 cm | 40 cm | Common size for standard pallets |
| 90 x 150 cm | 60 - 65 cm | 50 cm | Tall pallets, stacked two high |
| 100 x 180 cm | 70 - 75 cm | 60 cm | Machinery, large equipment |
| 120 x 240 cm | 85 - 90 cm | 70 cm | Oversized voids |
A gap wider than the maximum of the largest bag size should not be filled with a single bag. Narrow the gap with rigid filler such as empty pallets, thick carton dividers or honeycomb board first, and then place the bag. Otherwise the bag swells almost round, very little flat surface touches the cargo, the holding force drops sharply and pallet edges easily cut the bag. The Union Pacific railroad loading guide does the same: a standard bag for gaps of 10 to 30 cm, a square-type bag for gaps of 30 to 60 cm, with honeycomb board added on both sides.
On the other hand, if the gap is too narrow for the bag size, the bag cannot swell enough to build pressing force: it reaches its pressure while still flat and gives no cushioning. A gap of only a few centimetres is usually handled by repacking the cargo tighter or using a thin blocking board, with no need for a dunnage bag.
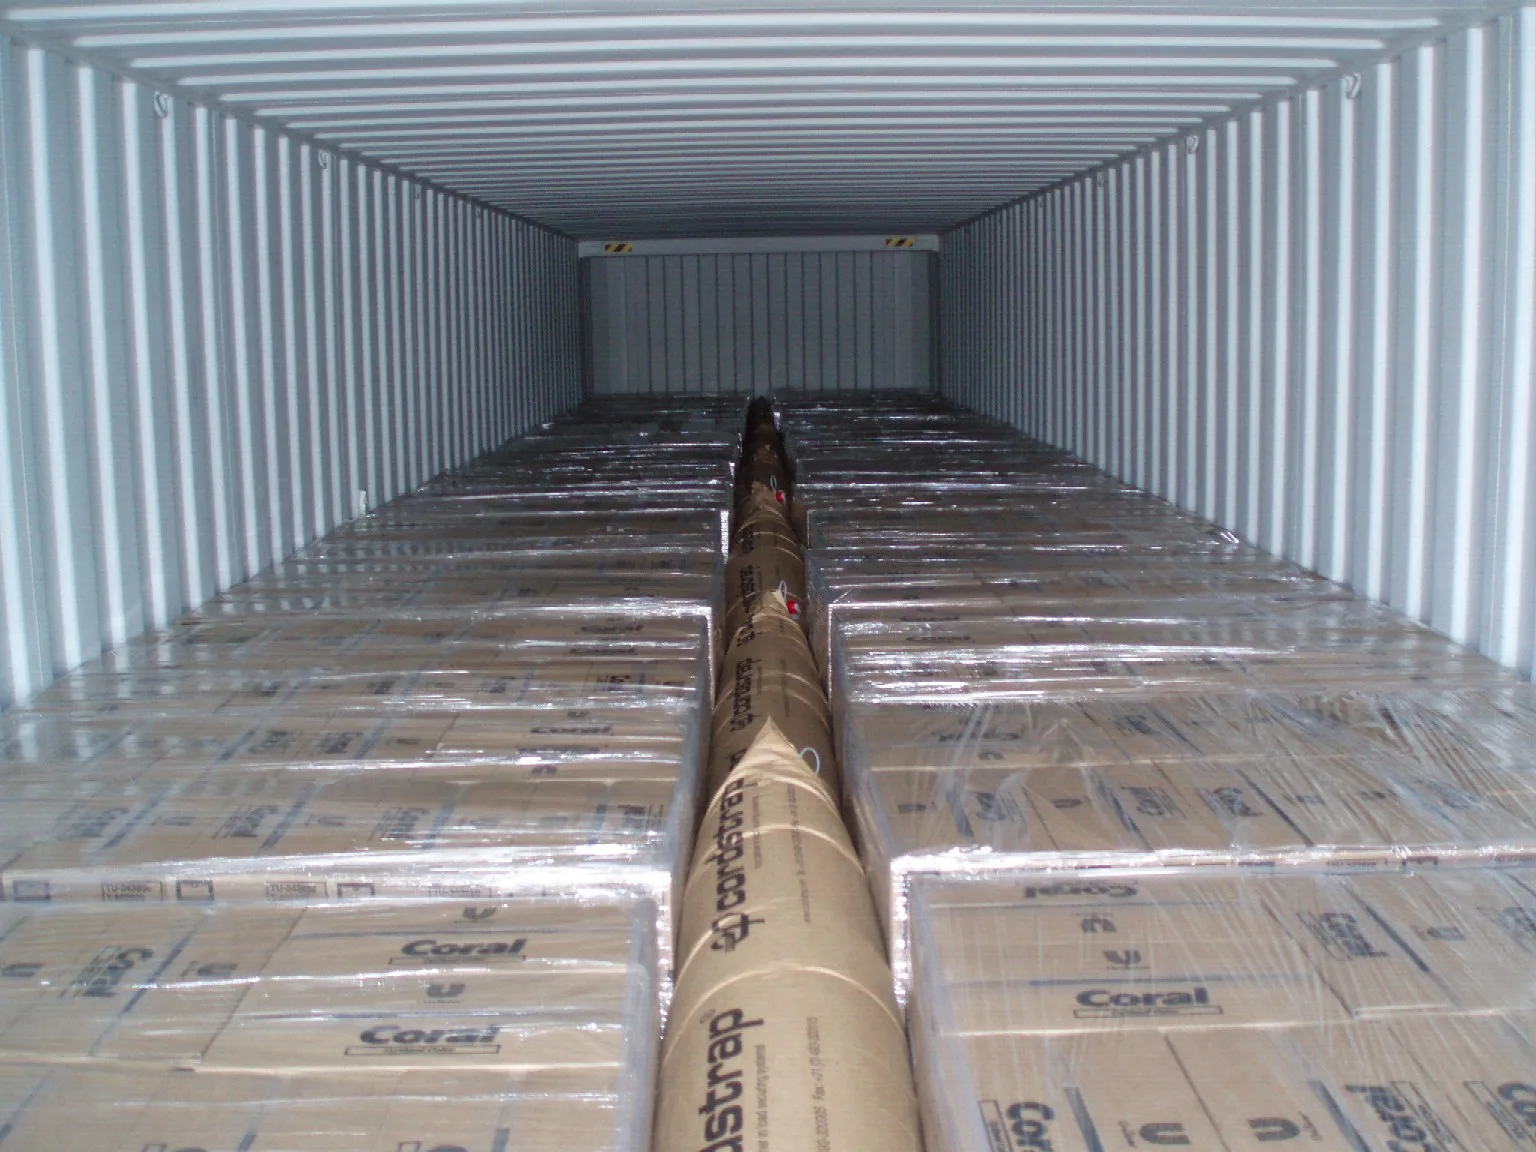
Preparing the environment and the padding
Kraft paper bags should be kept somewhere dry before use, because paper that absorbs moisture loses mechanical strength. Padding boards should be cut in advance from stiff carton, honeycomb board or thin plywood, large enough to cover sharp edges and spread the pressing force evenly over the face of the cargo. The CTU Code also says that rough cargo surfaces must be smoothed with padding before the bag is placed.
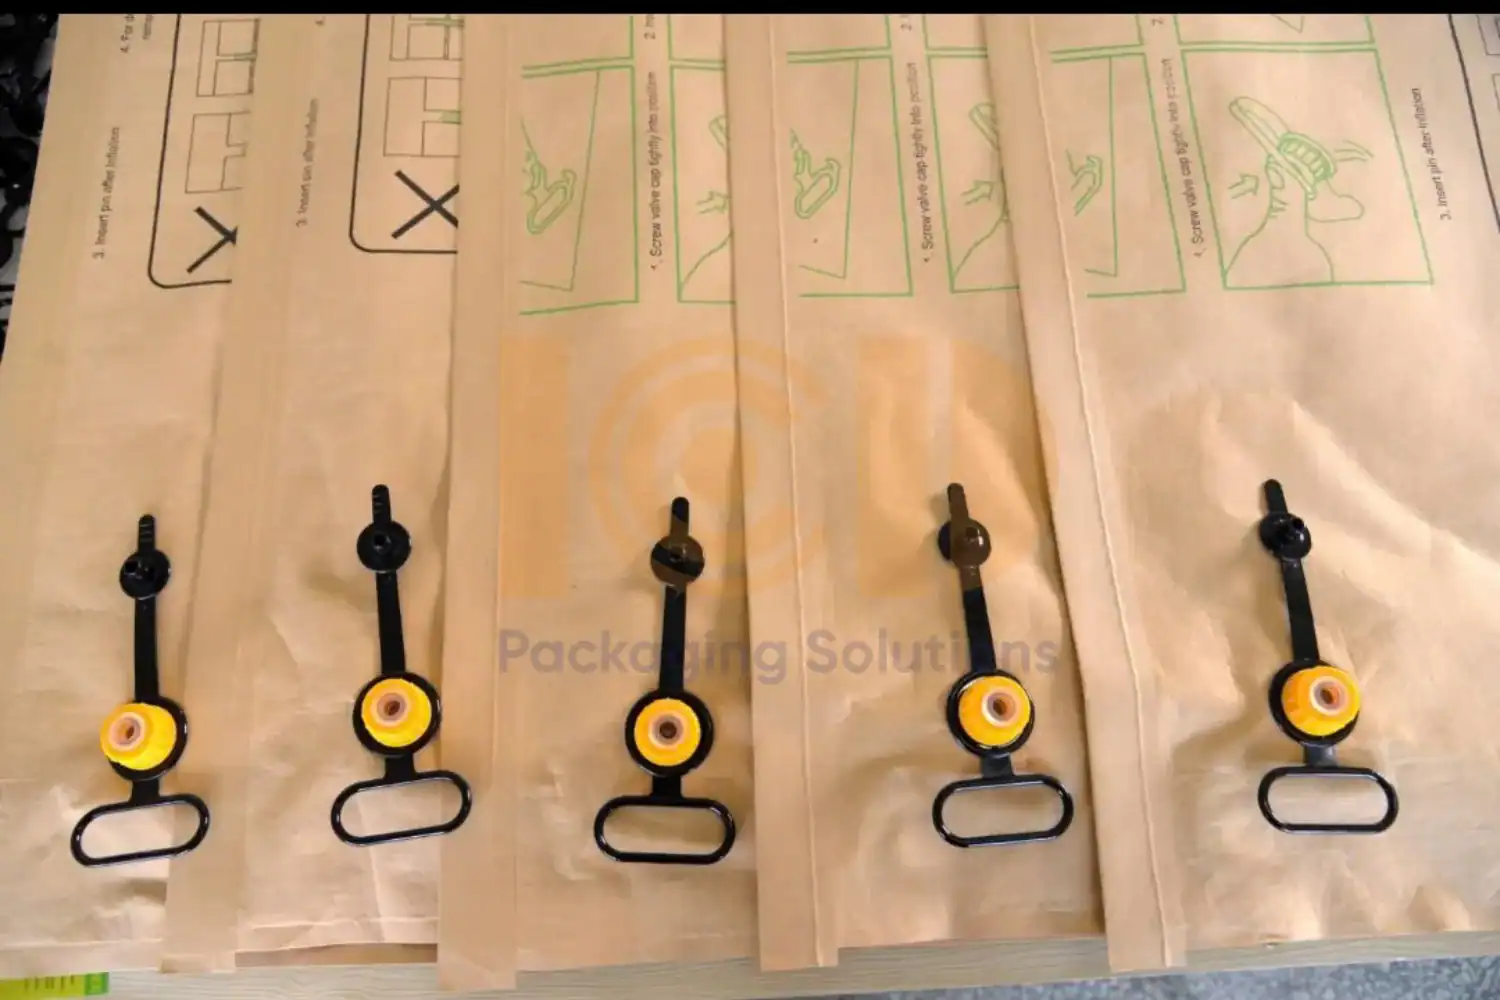
The 5-step procedure for container dunnage bags (Kraft and woven PP)
The procedure below applies to load-bearing dunnage bags used to secure cargo in containers, trucks or rail cars. Follow the order: pad, place, connect the gun, inflate, close the valve and check. If you use several bags in the same container, finish loading all the cargo first and only then inflate, so you do not have to deflate a bag to adjust it.
Step 1: Put in padding and protect sharp edges
Padding is a mandatory step, because a torn bag is the most common reason blocking fails. Put thick carton, honeycomb board or thin plywood wherever the bag will touch a sharp edge, the sharp corner of a wooden pallet, a metal box, nail heads or protruding parts of machinery.
Padding protects against two different kinds of failure. The first is a puncture from a hard hit on a sharp corner. The second is abrasion: constant vibration over the whole trip makes an edge slowly cut into the bag shell. This one is harder to see, because the bag may still be taut when the door is closed and only go flat after a few days at sea. A stiff pad spreads the force over a wide area and so reduces both.
Step 2: Place the dunnage bag in the gap
Put the bag in the middle of the gap to be filled, straight, not twisted, with no folded edges, and with the valve facing the person working so the inflation gun is easy to connect. The bag must lie completely between the two cargo faces; a bag edge sticking out past the load will swell unevenly and is easily cut.
The bag height should be close to the height of the load to be held, but not above the top edge of the cargo, so the bag holds the upper part of the units too. A bag placed too low holds only the base of the units, and when the container sways hard sideways the top can still tip. In my experience, after inflation the face of the bag should cover at least about half of the face of the cargo; the smaller the contact area, the lower the holding force even when the pressure is correct.
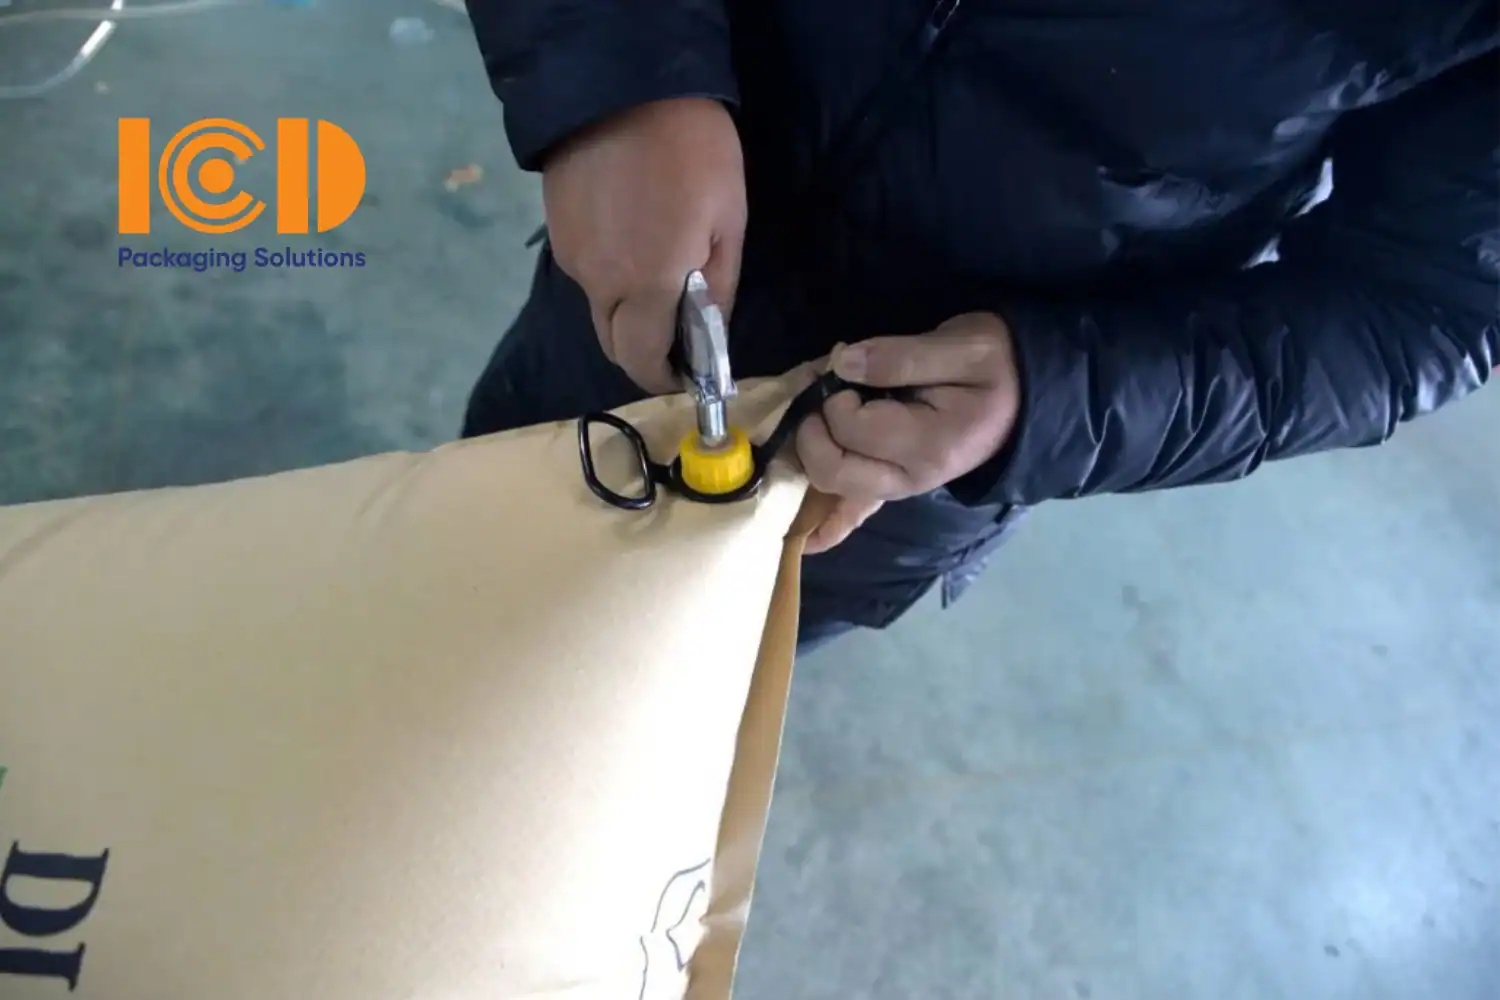
Step 3: Connect the inflation gun and control the pressure
A dedicated compressed-air gun with a pressure gauge is a condition for inflating to the right level. Inflation pressure follows the manufacturer’s recommendation for each bag level; for a Level 1 Kraft paper bag in the ICD Vietnam catalogue the working pressure is 0.2 bar (2.9 PSI), while higher-level bags have their own value printed on the specification sheet.
Connect the gun to the right valve type: a gun for quick-fill valves should not be used on small valves and the other way round, because a mismatched nozzle easily pierces the valve film. Inflate steadily until the bag is taut, lies flat against both cargo faces and the gauge reaches the recommended level, then stop. When two bags block both sides of a row of cargo, inflate them alternately, a little at a time, so the row is not pushed to one side.
Do not inflate until the bag is as hard as a rock. A correctly inflated bag still has some give: when the load pushes into it, the bag yields a little and then pushes back, which reduces the impulse passed into the cargo. A bag that is too hard passes almost the whole impact on to the cargo, and may also burst when the container heats in the sun and the air in the bag expands.
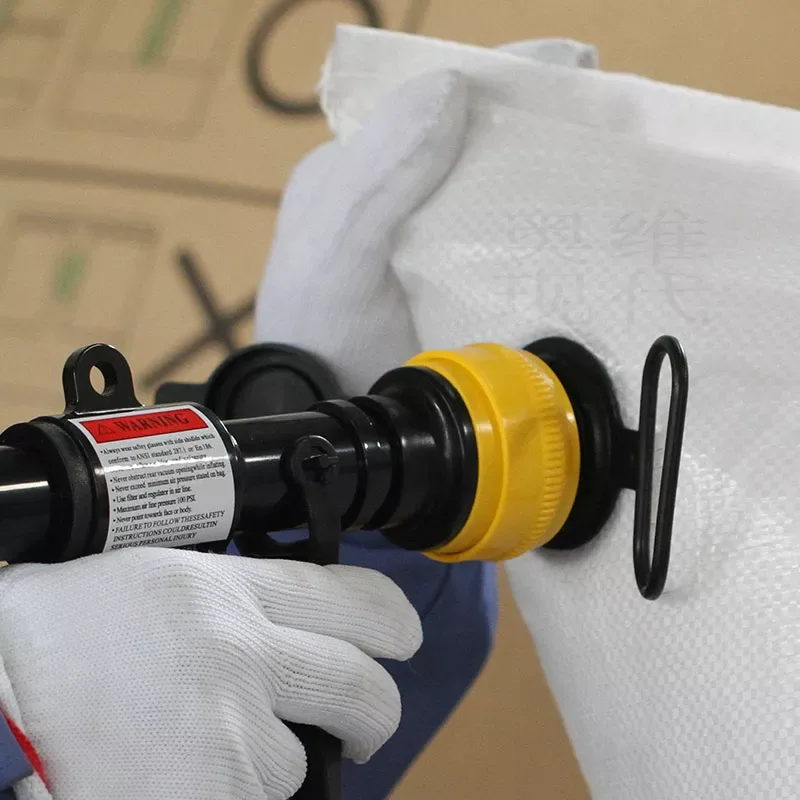
Step 4: Close the valve and check
After reaching pressure, pull out the inflation gun and listen at the valve. A good valve closes at once, with only a very short hiss as the gun is withdrawn; if the hiss goes on, the valve is not sealed or the valve film is damaged, and you need to re-inflate or replace the bag before loading continues.
Next, screw the valve cap on tight. The valve is the main air barrier and the cap is the second layer of protection, keeping the valve core from being knocked open during the journey. In my experience, walk around once and press every bag by hand again a little while after inflation, before closing the container door; a bag that has clearly gone soft is leaking, and replacing it while still in the warehouse is far easier than after the cargo has reached the port.
Step 5: Deflate and handle the bag after transport
Deflate before unloading to release the pressing force, otherwise cargo can spring out as soon as the first unit is removed. With a quick-fill valve, open the valve cap or use the reverse suction nozzle of the inflation gun to draw the air out; with no gun, open the cap and lay the bag on a flat surface so the air escapes by itself.
Woven PP bags can be reused many times if they pass inspection. Check the whole bag face under strong light for small tears, holes or worn spots, then inflate it and leave it for a day to see whether it still holds air. Kraft paper bags are normally used once on a long journey and should be discarded after the trip.
How to use carton void-fill air bags (light loads)
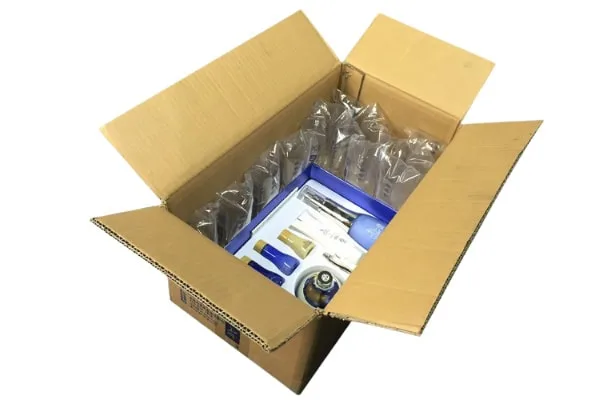
Carton void-fill air bags are used to cushion inside a box, not to secure a load in a container, so the method is quite different. They come as pillows or chains of PE or LLDPE film and are often used for e-commerce goods, cosmetics, glass bottles and ceramics.
Purpose and the rule of filling
The purpose is to keep fragile products from shaking and from hitting the walls of the box. The bags are inflated on the spot with a small electric pump running at low pressure, far safer than industrial compressed air. The bag only needs to be moderately taut to act as a soft cushion; over-inflated, it loses its cushioning and may even crush the delicate item itself.
How to fit: cushion around the product
Use chain-type air cushions or large bubble film to wrap around the product and protect every side. In my experience, always make an air cushion layer about 3 to 5 cm thick at the bottom of the box before putting the product in, because the bottom of the box takes the hardest impact when a parcel is thrown or dropped.
Then use pillow-type bags to fill the remaining gap above and on both sides. Shake the box gently: if the product no longer moves, it passes. The aim is to give every side of the product a cushion, so the impulse is spread out instead of landing on one corner.
Common mistakes when using dunnage bags
The two mistakes I meet most often are under-inflating container bags and reusing PP bags without inspection. Neither makes the bag fail at the moment of packing, so the packer usually does not know the mistake until feedback arrives from the destination port.
Under-inflation
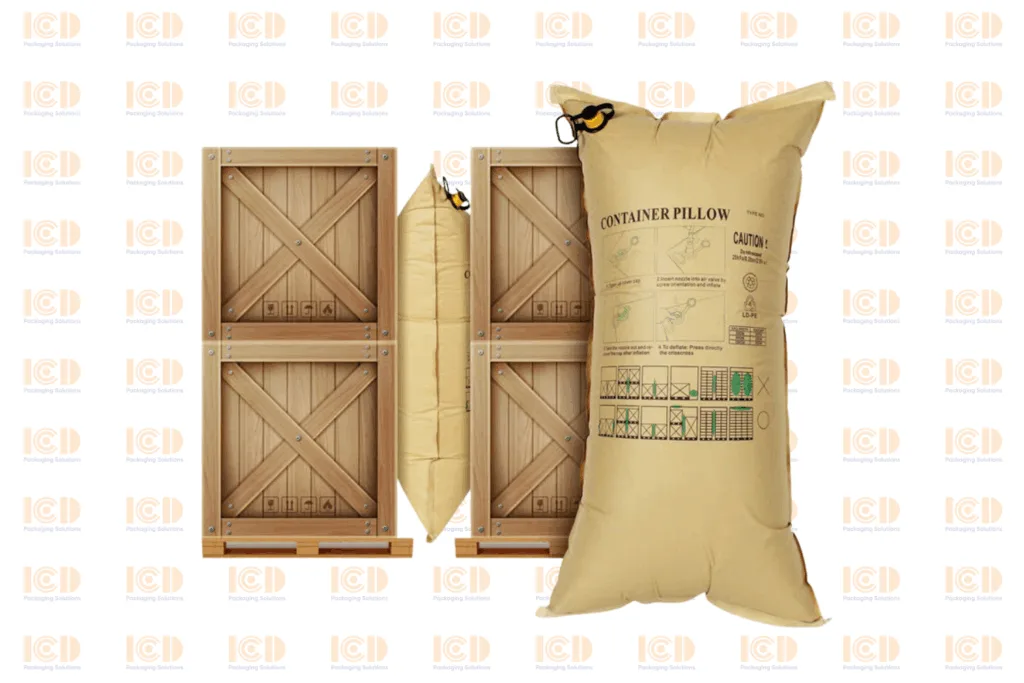
Many incidents come from under-inflation. A Level 1 bag inflated to only about 0.1 bar, half the recommended level, is easily compressed when the vehicle brakes hard, the load has room to build speed and every impact is harder than the last. The simple way to avoid it is to always use an inflation gun with a gauge and give the packer the specific number for each bag level.
Reusing woven PP bags
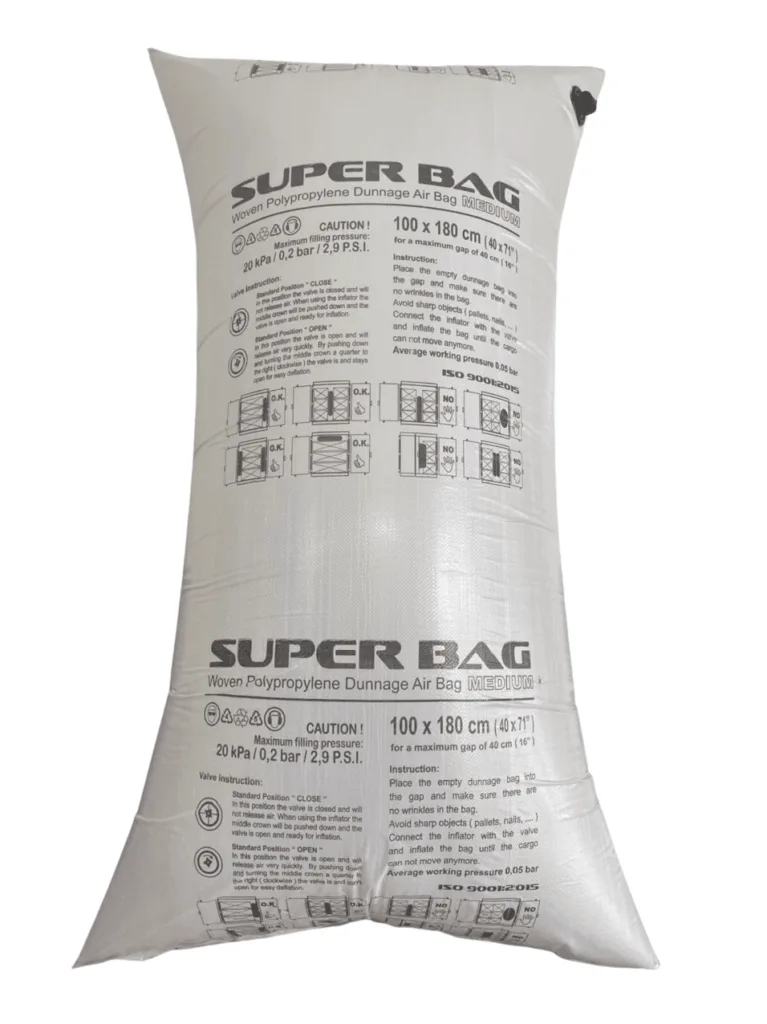
Woven PP bags can be reused but need a clear inspection routine. Each time a bag comes back, check its surface under strong light, look closely at the area around the valve and the sewn edges, and discard any bag with tears or deep wear at once. A bag that has lost quality but is put back into use will no longer hold its original strength level, and the CTU Code uses a lower safety factor for reusable bags than for single-use bags (0.5 compared with 0.75) precisely because of this risk.
Frequently asked questions about using dunnage bags
Do I need a pressure gauge when inflating a dunnage bag?
Yes. For container bags made of Kraft paper or woven PP, use an inflation gun with a gauge. Inflating by feel is the most common mistake and usually leads to under-inflation: the bag does not have enough static pressing force to hold the cargo, and the cargo can shift under braking or sideways sway.
Can a Kraft paper dunnage bag be reused?
Technically it can be re-inflated, but it should not be reused for long and harsh journeys such as sea or rail transport. Kraft paper weakens after each compression and exposure to moisture, so the risk of tearing or leaking is higher on the next trip. The type designed for repeated use is the woven PP bag.
How do I protect a dunnage bag from the sharp edges of a wooden pallet?
Always put a layer of padding between the bag and the sharp contact point, usually thick carton, honeycomb board or thin plywood. The padding spreads the pressing force evenly and stops the bag from being punctured by a hard hit or worn through by vibration over the whole trip.
Can a dunnage bag burst when the container sits in the hot sun?
The risk is low if the bag was inflated to the recommended pressure from the start, because the burst pressure is about three times the working pressure according to the ICD Vietnam catalogue (Level 1: 0.2 bar working, 0.6 bar burst). The risk rises when the bag is over-inflated, because the air in the bag expands further as the container heats up.
Can I use a bicycle or motorbike pump to inflate a dunnage bag?
No. A container bag needs a large volume of air and fast inflation; a hand pump takes a very long time and cannot control the pressure. Use a compressed-air source (an air compressor) with a dedicated gun that fits the bag valve.
How much wider than the gap must the bag be?
There is no single ratio for every bag; check the maximum gap table for each bag size. For example, according to the ICD Vietnam product page, an 80 x 120 cm paper bag is for a maximum gap of 40 cm and a 100 x 180 cm bag for a maximum gap of 60 cm. Many people apply a rule that the bag should be 2 to 3 times wider than the gap; that rule gives a rough result, but the manufacturer’s table remains the main reference.
Can I put a dunnage bag at the container door?
It is not recommended. The CTU Code advises against using air bags to fill the void next to the door unless you are sure the door will not be forced open when it is unlocked. A gap at the door should be blocked with timber, a blocking frame or straps.
Contact us for technical advice and to buy dunnage bags
ICD Vietnam supplies Kraft paper dunnage bags, woven PP bags, carton void-fill air bags and quick-fill valve inflation guns. Send us the gap size, the type of cargo and the shipping route; our advisers will recommend the level, the bag size and the layout. Price: contact for a quote.
ICD Vietnam Industrial Manufacturing Co., Ltd.
- North Vietnam (Hanoi warehouse): 3rd Floor, Thang Long A1 Building, Thon Bau, Thien Loc Commune, Hanoi - 0983 797 186 / 090 345 9186 / 090 5859 186.
- Southern workshop: 551/212 Le Van Khuong Street, Tan Thoi Hiep Ward, District 12, Ho Chi Minh City - 098 6784 186.
- Email: sales@icdvietnam.com.vn. Zalo: Chat Zalo.
References
- How to use a dunnage bag correctly: International Safe Transit Association (ISTA).
- IMO/ILO/UNECE Code of Practice for Packing of Cargo Transport Units (CTU Code), MSC.1/Circ.1497 - Annex 7 section 2.3 (air bags: follow the manufacturer’s instructions, do not use at the door, smooth the surface), Appendix 4 (safety factor).
- Union Pacific - Air Bag Placement and Usage Guidelines for Securing Intermodal Pallet Loads.
- ICD Vietnam air dunnage bag catalogue (level table, working pressure and burst pressure) and the size and maximum gap table on the ICD Vietnam Kraft paper air bag product page, consulted October 2026.