
Table of Contents
- What stages does plastic crate manufacturing include?
- What resin are plastic crates made from?
- Which plastic crates does injection moulding produce?
- What technology makes plastic drums, jerry cans and IBC tanks?
- What crates do rotational moulding, thermoforming and Danpla sheet fabrication make?
- Which technology for which type of crate?
- How are plastic crates finished and inspected before delivery?
- Now that you know the process, what should you ask when ordering plastic crates?
- Frequently asked questions about plastic crate manufacturing technology
- What technologies make industrial plastic crates?
- What machine makes plastic crates?
- What steps does plastic crate manufacturing involve?
- Should plastic crates be made from HDPE or PP?
- Why do crates of a custom size often have to be ordered in large quantities?
- Can crates made from recycled resin be used?
- How do injection-moulded crates differ from Danpla boxes?
- Do plastic crates bought from ICD Vietnam carry a warranty?
- Contact us about plastic crates
- References
Reviewed and updated by ICD - Week 46/2026
Plastic crates are made in three stages: preparing HDPE or PP resin together with colour masterbatch and additives; forming with the technology that suits the crate type (injection moulding for solid crates and open-wall crates, blow moulding for drums and jerry cans, rotational moulding for large tanks, thermoforming for thin trays, sheet fabrication for Danpla boxes); and then finishing and inspection.
I am Le Van Thang and I have worked at ICD Vietnam since 2011. When I advise on plastic crates, a question I am often asked is why two crates that look almost the same differ in price and strength, or why a crate of a custom size must be ordered in large quantities. Most of the answer lies in how the crate is made: which resin is used, which forming technology and how it is inspected.
This article follows that same order, from resin to finished crate, and shows which crate type goes with which technology. The step-by-step detail of one injection moulding cycle is in a separate article on injection moulding of plastic crates on the ICD blog, so here I only summarise. The plastic crates on the ICD website are also divided into these groups, so you can cross-check as you read.
What stages does plastic crate manufacturing include?
Every plastic crate goes through the same three stages: preparing the raw material, forming in a mould or from plastic sheet, and finishing and inspection before leaving the factory. The biggest difference between crate types lies in the second stage.
The forming technology decides whether a crate is solid or hollow, thick-walled or thin, how accurate its dimensions are and how much the mould costs. That is why understanding the plastic crate manufacturing process helps a buyer read the specifications correctly and ask the right questions when ordering. Among the types of plastic crates on the market, solid crates, open-wall crates and pallet boxes make up most of the volume and are almost all injection moulded; liquid containers such as drums and jerry cans use blow moulding.
What resin are plastic crates made from?
Industrial plastic crates are mostly made from two thermoplastics, HDPE and PP: HDPE is tough and resists impact well in the cold; PP is stiffer and lighter and tolerates higher temperatures. Both melt when heated and harden when cooled, so they can be used for injection moulding, blow moulding and rotational moulding.
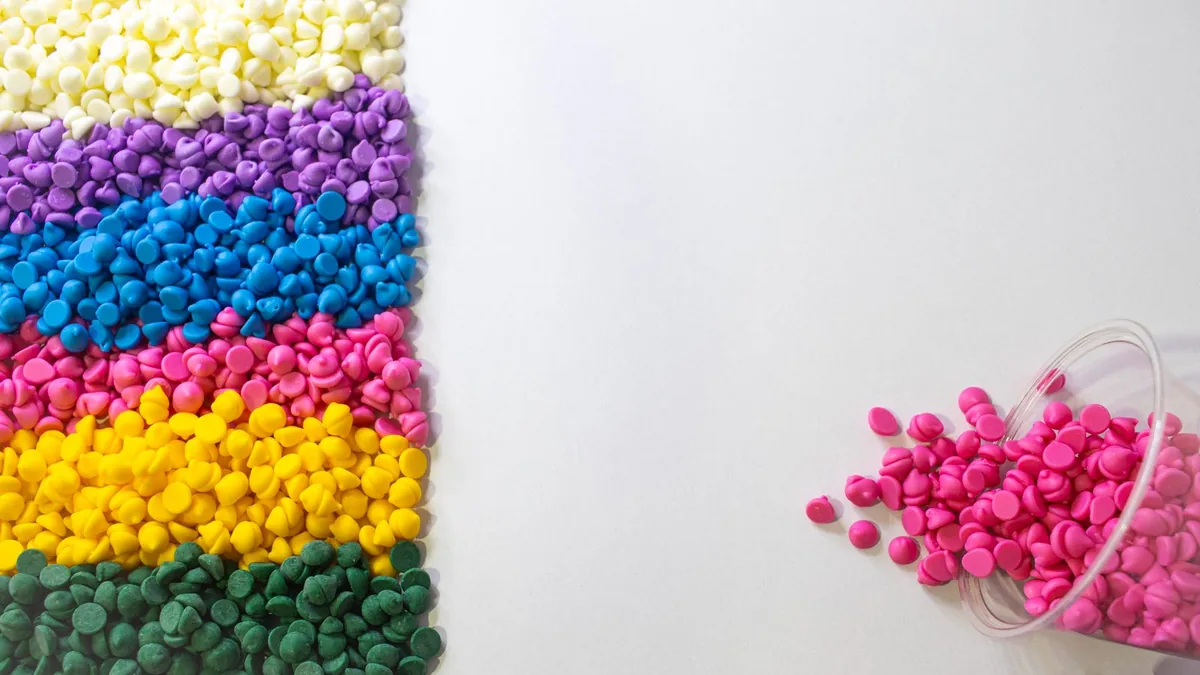
Besides the main resin, the formulation usually contains colour masterbatch for even colour and a UV-resistant additive for crates used outdoors, because sunlight makes plastic brittle and faded quickly. Another important variable is the share of recycled resin. Recycled resin lowers the price, but its strength and colour consistency are harder to keep stable than virgin resin, and crates for food usually have to use virgin resin. When comparing prices of two crates of the same size, first ask clearly about the material and the share of virgin resin.
Of the 117 plastic crate codes listed on the ICD Vietnam website (counted on 16 October 2026), 55 codes list PP and HDPE, 44 codes list PP only, 5 codes list HDPE only, and the rest do not state the material clearly or use another material. The table below summarises the differences between the two resins:
| Criterion | HDPE | PP |
|---|---|---|
| Melting point (for reference) | About 120 - 140 °C | About 160 - 170 °C |
| Advantages | Tough, resists impact well at low temperatures | Stiffer, lighter, tolerates higher temperatures |
| Common technologies | Injection moulding, blow moulding (drums, jerry cans), rotational moulding | Injection moulding, extruded Danpla sheet |
| Best for | Open-wall crates, cold-store crates, drums, chemical jerry cans | EU-standard crates, component trays, Danpla boxes |
| Codes on the ICD website (16 October 2026) | 5 codes HDPE only | 44 codes PP only; 55 codes list both PP and HDPE |
For crates used in cold stores or crates that are often knocked during loading, HDPE is usually safer. For crates that must be rigid, deform little when stacked high or must be washed with hot water, PP is the common choice.
Which plastic crates does injection moulding produce?
Injection moulding is the most common technology for industrial plastic crates: solid crates, open-wall crates, pallet boxes, component trays and EU-standard crates are all injection moulded, because the process gives even thick walls, accurate dimensions and high volumes.
An injection moulding machine has three main units: the injection unit, the mould and the clamping unit. Resin pellets pass from the hopper into a heated barrel, where a screw both rotates and melts and mixes the resin, pushing forward just enough for one shot. The screw then advances like a piston, forcing the resin into the mould cavity at high pressure and speed, with an injection time usually under 1 second. According to the Injection moulding entry on Wikipedia, the machine switches to the hold-pressure phase when the cavity is about 95 - 98% full to compensate for shrinkage, and then cooling water runs through the mould until the crate is rigid enough to eject.
Solid plastic bins have thick walls and a closed base, and are used to carry heavy goods in seafood, garment and food businesses. Open-wall crates have mesh walls so the goods can breathe. Pallet boxes are large crates with feet or runners for forklifts. All three groups need to stack tightly many tiers high, and that is why they are almost always injection moulded rather than made with another technology.
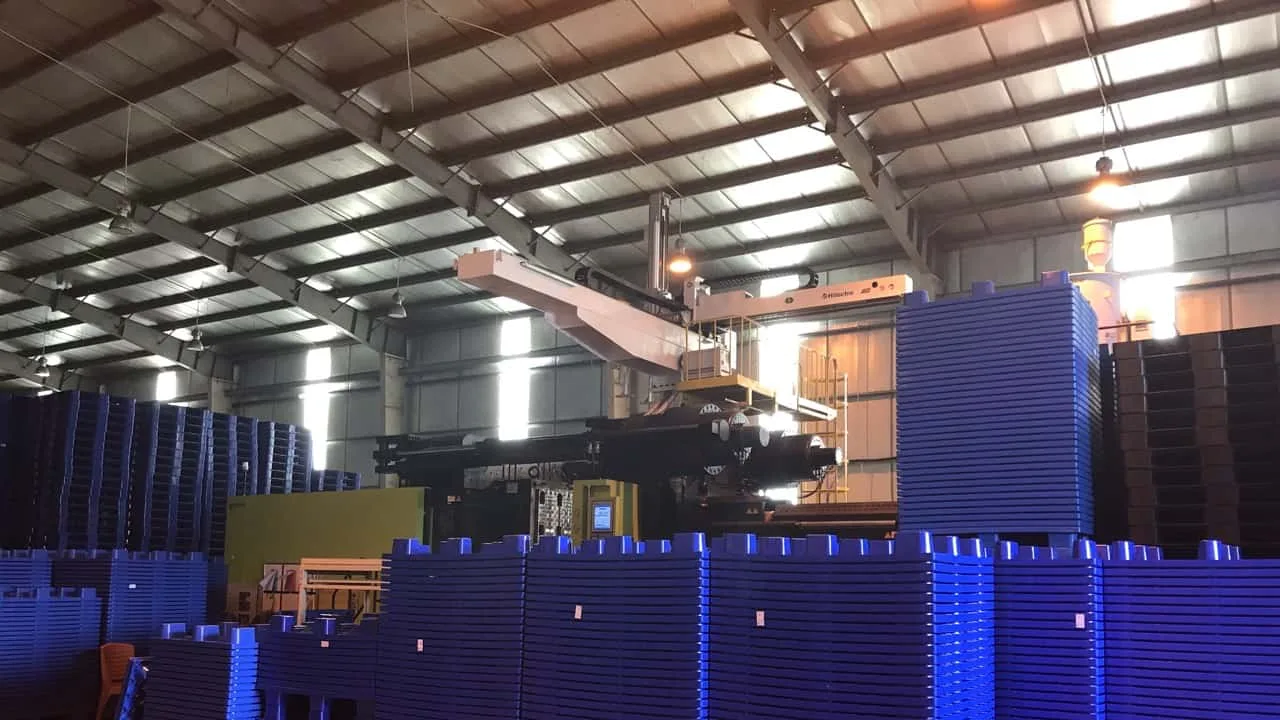
The point a buyer most needs to know about injection moulding is the mould cost. Injection moulds are usually made of steel, precisely machined, and many steel mould sets are designed to run more than a million products over their life. Moulds are expensive, so this technology only pays off at high volume: standard crate codes have good prices because the mould cost is spread thin, while crates of a custom size usually come with a minimum order quantity.
What technology makes plastic drums, jerry cans and IBC tanks?
Plastic drums, jerry cans and the inner bottle of an IBC tank are made by blow moulding, the technology that specialises in hollow, watertight, large-capacity products that injection moulding cannot make in one go.
With extrusion blow moulding, the type commonly used for drums and jerry cans, molten plastic is extruded into a soft tube called a parison. A two-half mould closes around the parison, and compressed air is blown in to inflate the tube against the mould wall. When the plastic cools and hardens, the mould opens and the product is removed, and the excess plastic at the neck and base is trimmed off and ground for reuse. An IBC tank is a blow-moulded plastic bottle held in a steel cage frame, so when buying a tank you need to ask separately about the bottle and the frame.
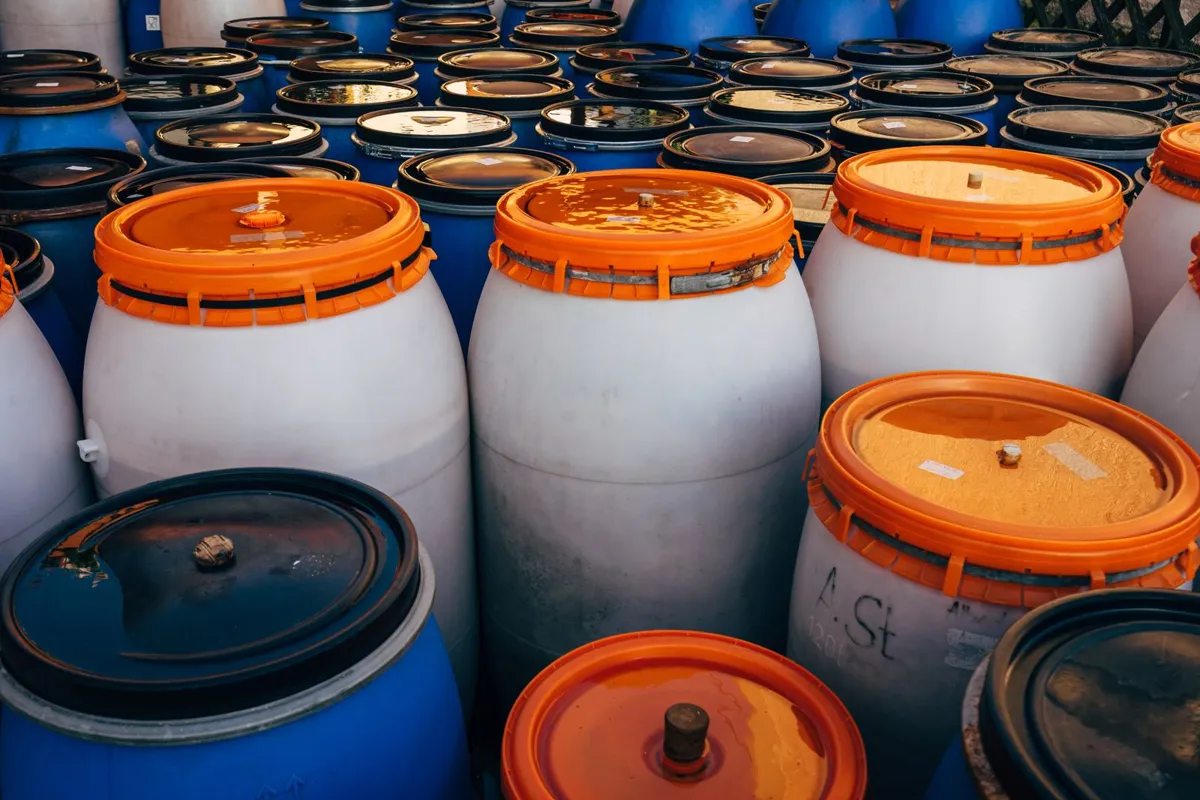
A blow mould only withstands compressed air pressure far lower than injection pressure, so it is usually cheaper than an injection mould of the same size, but absolute wall-thickness uniformity is hard to achieve. That is why for drums and jerry cans, the product weight and the thickness at the corners are two figures worth asking about when comparing.
What crates do rotational moulding, thermoforming and Danpla sheet fabrication make?
These three technologies cover the rest of the market: rotational moulding for very large tanks and hollow crates, thermoforming for thin-walled trays and boxes, and sheet fabrication for Danpla boxes in many sizes; what they share is lower mould cost than injection moulding.
Rotational moulding puts plastic powder into a metal mould, heats it and slowly rotates the mould about two perpendicular axes so the plastic coats the walls evenly, then keeps rotating while it cools so the product does not sag. No high pressure is needed, so aluminium or sheet-steel moulds are cheaper, but the cycle is long. Thermoforming starts from plastic sheet: the sheet is heated until soft, drawn by vacuum or pressed by air into a mould and then trimmed; thin sheet makes trays and containers, while thick sheet can make large parts such as plastic pallets.
What these groups share is that they suit large products, many different sizes or moderate quantities. In return, dimensional accuracy and speed are not as good as injection moulding, so they are rarely used for crates that must be stacked automatically with tight tolerances.
Which technology for which type of crate?
A quick rule: solid, stackable, high-volume crates use injection moulding; hollow liquid containers use blow moulding; very large tanks use rotational moulding; thin trays use thermoforming; many sizes in small quantities use Danpla sheet fabrication.
| Technology | Typical crate | Shape and walls | Mould cost | Suitable volume |
|---|---|---|---|---|
| Injection moulding | Solid crates, open-wall crates, pallet boxes, component trays | Open top, even thick walls, accurate | Highest | Large, stable for many years |
| Blow moulding | Drums, jerry cans, IBC bottles | Hollow and sealed, thinner walls at the corners | High, lower than injection moulding | Large |
| Rotational moulding | Storage tanks, large waste bins, large insulated boxes | Hollow, very large sizes | Low to medium | Small to medium |
| Thermoforming | Trays, thin-walled boxes | Shallow, thinnest at the corners | Low | Very large (packaging) or medium |
| Danpla sheet fabrication | Divided boxes, component boxes, antistatic boxes | Cut, folded and joined from hollow PP sheet | Almost no mould needed | Small to medium, many sizes |
This table explains a common situation when ordering: for the same 600 x 400 mm crate, an injection-moulded model with an existing mould is cheap and quick to deliver, while a model in a custom size needs a new mould and only makes sense in large quantities, or must switch to a Danpla box if the quantity is small.
How are plastic crates finished and inspected before delivery?
After leaving the mould, the crate is trimmed of flash, fitted with a lid, hinges, handles or latches if any, printed with a logo or labelled as required, then checked for size, weight, appearance and a stacking test. The crate’s weight is the simplest figure that shows whether it has enough plastic.
The detailed quality control process is in a separate article on the ICD blog. For a buyer, it is enough to know the five faults most often seen in injection-moulded crates so you can check a batch as soon as it arrives:
- Short shot: a wall or rib is missing because the mould did not fill completely.
- Sink mark: a slight dent on the surface opposite a rib or a foot.
- Warping: a twisted base or wall, so crates do not stack tightly.
- Flash: a thin layer of plastic spilling out at the parting line of the two mould halves.
- Weld line: a fine mark where two plastic flows meet, which cracks easily on impact.
A small tip: weigh a few crates of the same code at random from the batch. If the weights differ noticeably, it is a sign that the moulding process is unstable or the resin has changed, so tell the supplier before putting the crates into use.
Now that you know the process, what should you ask when ordering plastic crates?
The four questions worth asking before you order plastic crates all follow from the process above:
The answers to these four questions are enough to compare two quotes fairly, rather than comparing only the final figure.
Frequently asked questions about plastic crate manufacturing technology
What technologies make industrial plastic crates?
Mainly injection moulding (solid crates, open-wall crates, pallet boxes), blow moulding (drums, jerry cans, IBC bottles) and thermoforming (trays, thin-walled boxes). There is also rotational moulding for large tanks and hollow crates, and fabrication from hollow PP sheet for Danpla boxes.
What machine makes plastic crates?
Solid crates and open-wall crates are made on an injection moulding machine with an injection unit, a mould and a clamping unit; the larger the crate, the greater the clamping force required. Drums and jerry cans are made on blow moulding machines, large tanks on rotational moulding machines and thin trays on thermoforming machines.
What steps does plastic crate manufacturing involve?
Three stages: preparing the raw material (HDPE or PP resin, colour masterbatch, additives), forming with a suitable technology, then finishing and inspection. For an injection-moulded crate, the forming stage consists of plasticising the resin, injecting into the mould, holding pressure, cooling and ejecting the crate.
Should plastic crates be made from HDPE or PP?
HDPE is tough and resists impact well in the cold, so it suits open-wall crates, cold-store crates, drums and chemical jerry cans. PP is stiffer, lighter and tolerates higher temperatures, so it suits EU-standard crates, component trays and Danpla boxes.
Why do crates of a custom size often have to be ordered in large quantities?
Because an injection-moulded crate needs its own steel mould, and the mould cost is high. Only when the volume is large enough does the mould cost per crate become reasonable. For small quantities, a Danpla box fabricated from sheet is usually the alternative because it needs almost no mould.
Can crates made from recycled resin be used?
They can be used for many jobs such as holding scrap or transporting goods with no hygiene requirement, but their strength and colour are harder to keep stable than virgin resin. Crates for food should use virgin resin, and buyers should ask clearly about the share of recycled resin before comparing prices.
How do injection-moulded crates differ from Danpla boxes?
Injection-moulded crates are made in one piece in a steel mould, with thick walls and good load-bearing and stacking. Danpla boxes are cut, folded and joined from hollow PP sheet; they are lighter, quick to change in size and suit small quantities, but carry a lower load.
Do plastic crates bought from ICD Vietnam carry a warranty?
Yes. ICD Vietnam plastic crates carry a 12-month warranty under the warranty and repair policy published on the website. For a model that needs a custom size, the ICD team will advise the closest available code or a custom-order option with a specific quantity and delivery time.
Contact us about plastic crates
ICD Vietnam Industrial Manufacturing Co., Ltd
For advice on choosing crates by goods, load and stacking method, please contact:
- Northern Vietnam: 0983 797 186 / 090 345 9186 / 090 5859 186.
- Southern Vietnam: 098 6784 186.
- Email: sales@icdvietnam.com.vn.
- Zalo: Chat with ICD Vietnam on Zalo.
ICD Vietnam plastic crates carry a 12-month warranty under the warranty and repair policy published on the website.
References
- Wikipedia, Injection moulding: machine structure, injection cycle, the 95 - 98% hold-pressure switchover point, steel mould life.
- Wikipedia, the entries Blow molding, Rotational molding and Thermoforming: principles of extrusion blow moulding, rotational moulding and thermoforming.
- Society of Plastics Engineers, SPE: technical resources on plastics processing.
- ICD Vietnam: number of codes and materials of plastic crates in the website product catalogue, counted on 16 October 2026.