Table of Contents
- What is thermoforming and how does it differ from other ways of shaping plastic?
- What steps does the thermoforming process include?
- Should you choose vacuum, pressure or plug-assist forming?
- How does sheet thickness matter and how is it calculated?
- Which plastics can be used for thermoforming?
- What parameters matter for a thermoforming mould?
- When should you use thermoforming instead of injection moulding?
- Frequently asked questions about thermoforming
- What is a thermoformed plastic?
- What steps does the thermoforming process include?
- How do vacuum forming and pressure forming differ?
- Which plastics are commonly used in thermoforming?
- How thick is thermoforming plastic sheet?
- Is thermoforming expensive?
- Why are thermoformed products thin at the corners?
- What parts does a thermoforming machine have?
- What is a vacuum-formed plastic tray?
- Can thermoforming make load-bearing plastic containers?
- Contact ICD Vietnam
- References
Reviewed and updated by ICD - Week 44/2026
Thermoforming is a way of softening a thermoplastic sheet by heating, then using vacuum, compressed air or a plug to press the sheet into a single-sided mould to form a 3D shape. Sheet under 1.5 mm makes trays, blister packs and boxes; sheet over 3 mm makes equipment housings, liners and plastic pallets. The tooling is cheaper than injection moulding, in exchange for walls that thin out at the corners.
I am Le Van Thang and I have worked at ICD Vietnam since 2011. Customers who buy our plastic containers sometimes ask about the divided liner trays that sit inside a container, or ask why a thin tray needs far cheaper tooling than a container of the same size. The answer lies in thermoforming technology. This article goes into that technology alone: choosing vacuum or pressure, calculating sheet thickness, choosing the plastic, designing the mould and when to use it instead of injection moulding.
What is thermoforming and how does it differ from other ways of shaping plastic?
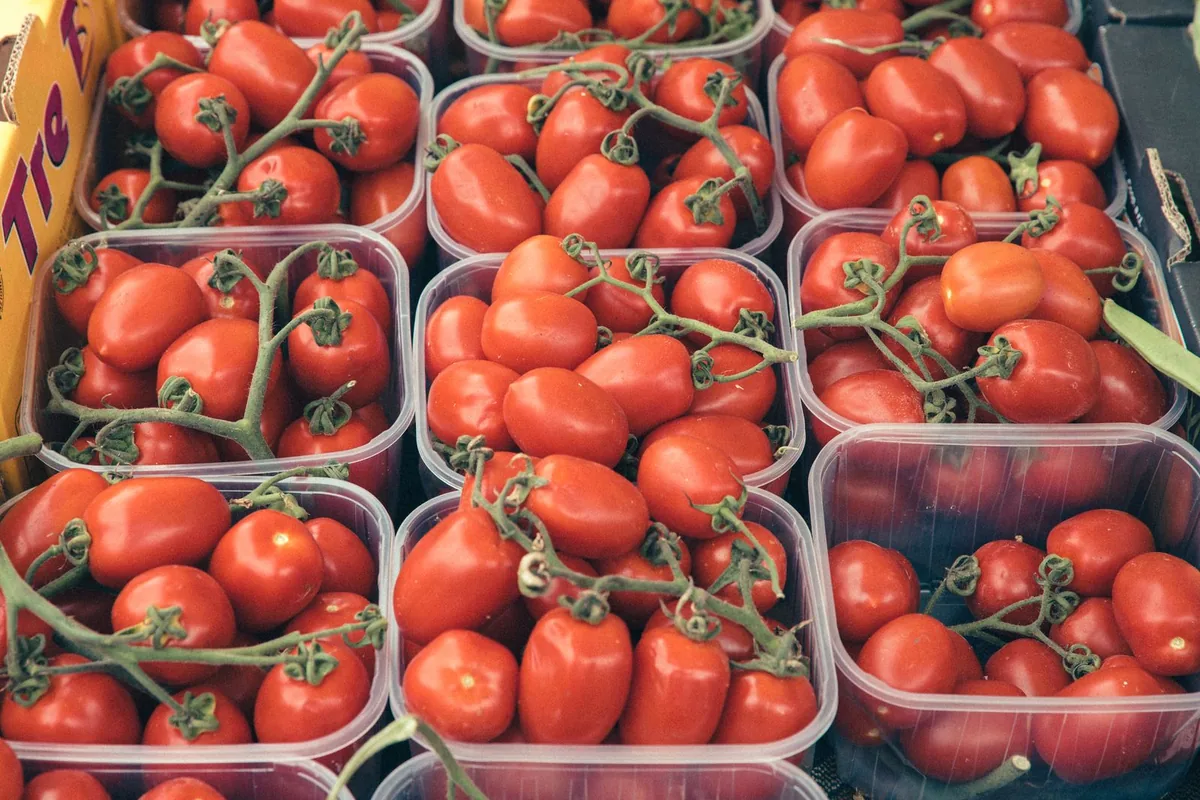
Thermoforming starts from a pre-extruded plastic sheet, not from plastic pellets, and needs only a single-sided mould. The sheet is heated to forming temperature, stretched onto or into the mould, held to cool and then trimmed. Because only one face of the product touches the mould, only that face has controlled dimensions; wall thickness varies with how far the sheet is stretched.
The Vietnamese terminology is rather mixed: “hut chan khong”, “nhua dinh hinh” and “tao hinh nhiet” all refer to the same family of technology. Vacuum forming is the simplest form; pressure forming, plug-assist forming and twin-sheet forming are variants. The overview article on plastic crate manufacturing technologies on the ICD blog already places thermoforming next to injection moulding, blow moulding and rotational moulding; here I go into it alone.
What steps does the thermoforming process include?
One thermoforming cycle has three main steps: heating the sheet, pressing the sheet into the mould with vacuum or compressed air, then cooling and trimming. Before that the sheet is clamped tightly in a frame so it does not shrink back when hot.
Step 1: heating the plastic sheet
The sheet is moved into the heating zone, with heavy gauge sheet usually heated on both sides, until it reaches forming temperature. Amorphous plastics such as PS, ABS and PETG have a wide forming temperature range and are easy to work. Semi-crystalline plastics such as PP and PE change very quickly from pliable to molten; according to guidance from machine maker Formech, PP has a forming window of only about 10 °C, so it needs precise temperature control and a sensor for sheet sag.
Formech gives an easy starting rule for a single-sided infrared ceramic heater: about 20 seconds for every 0.5 mm of thickness, so a 1.5 mm sheet needs about 60 seconds. PP and PE need longer, about 75 seconds for a 1.5 mm sheet. This is only a starting point; the operator still has to adjust for each batch of sheet and each heating zone.
Step 2: pressing the sheet into the mould
When the sheet is soft enough, the mould table rises or the sheet is lowered and a pump draws the air between the sheet and the mould through small holes in the mould. Atmospheric pressure pushes the sheet against the mould. For parts that need sharp corners or a crisp surface, shops add a pressure box above to blow compressed air down on the sheet; for deep parts, a plug first pushes the plastic toward the bottom of the mould before the vacuum is drawn.
Step 3: cooling, releasing and trimming
The product is held on the mould until it has cooled hard enough, usually with fans or water mist; an aluminium mould with cooling channels is faster. A puff of air blown back from the mould side helps release the product. Thin gauge items are cut with a die right on the machine; heavy gauge items are usually cut with a CNC router or hand tools. The excess sheet edge is ground to be extruded back into sheet.
Should you choose vacuum, pressure or plug-assist forming?
Choose vacuum for trays, blister packs and simple-shaped housings because the equipment and tooling are cheapest; choose pressure forming when you need sharp corners, raised lettering and a surface close to an injection-moulded part; add a plug assist when the part is deep. The reason lies in the forming force: vacuum cannot push the sheet harder than atmospheric pressure, about 1 atm.
| Method | How force is created | Advantage | Suited to |
|---|---|---|---|
| Vacuum forming | Draws air from between the sheet and the mould, maximum force about 1 atm (14.7 psi) | Cheapest equipment and tooling | Trays, blister packs, simple housings |
| Pressure forming | A pressure box blows compressed air onto the back of the sheet, usually up to about 50 psi (3.4 bar) | Sharp corners, surface detail close to injection moulding | Equipment housings, parts that need good appearance |
| Plug assist | A plug pushes the sheet into the female mould before vacuum or air pressure | More even thickness on deep draws | Cups, deep boxes, deep multi-cavity trays |
| Twin-sheet | Two hot sheets form on two opposing moulds and are welded closed at the edges | Hollow double-wall parts | Hollow parts, lightweight structural panels |
Air pressure levels differ by material and mould. The ACRYLITE acrylic sheet forming handbook states that air pressure is usually no more than 50 psi, and in some cases up to 200 psi. Moulds for pressure forming therefore have to be as rigid as a pressure vessel, usually aluminium, more expensive than a vacuum mould but still cheaper than a steel injection mould.
How does sheet thickness matter and how is it calculated?
Sheet thickness splits thermoforming into two branches: sheet under 1.5 mm is fed from a roll and runs on continuous high-speed machines; sheet over 3 mm is fed as pre-cut individual sheets. The 1.5 to 3 mm range is a medium gauge branch, small but growing, according to the classification on Wikipedia.
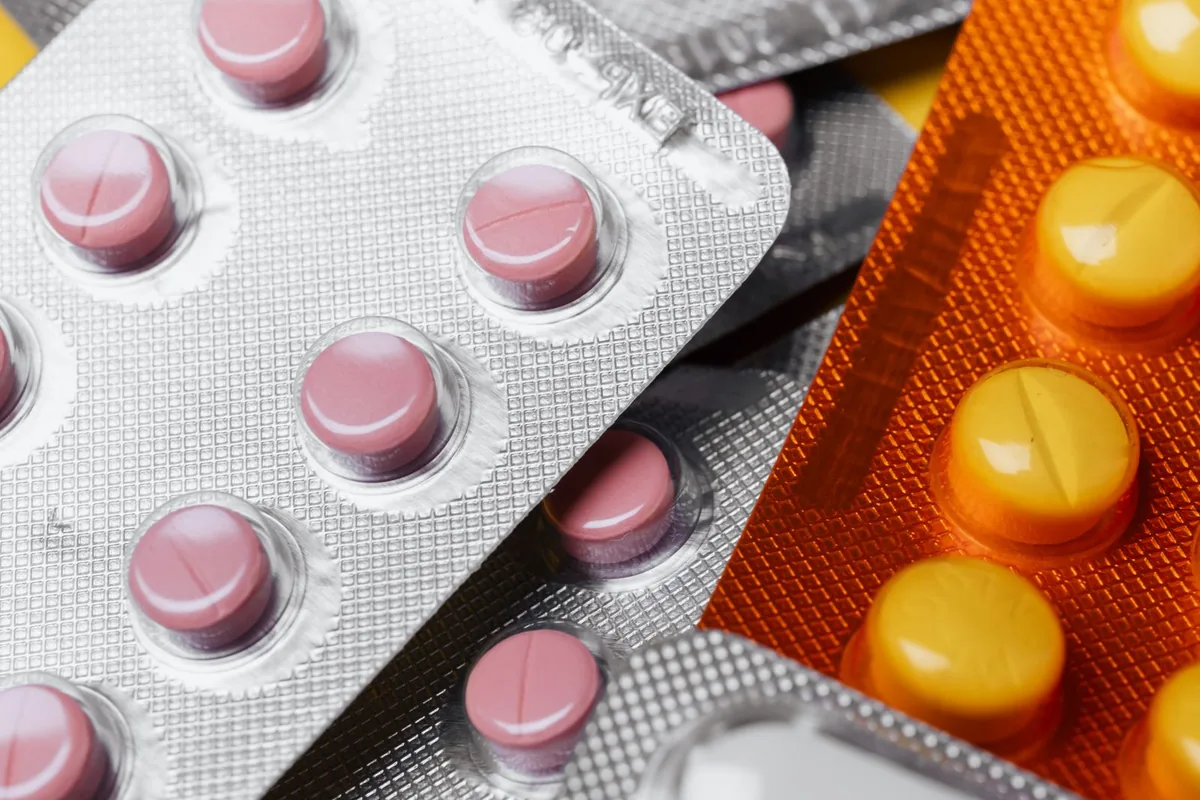
The thin gauge branch is almost entirely packaging: cups, boxes, lids, trays, medicine blister packs and clamshells for food, medical and retail. The heavy gauge branch makes long-life parts such as car door panels, refrigerator liners, small truck bed liners and also plastic pallets. Heavy gauge parts are usually made in volumes of 250 to 3,000 pieces a year, where cheap tooling and fast prototyping are a big advantage over injection moulding.
To choose the starting sheet thickness, use the draw ratio, equal to the product surface area divided by the opening area. The minimum sheet thickness is approximately this ratio multiplied by the desired wall thickness. For example, a 400 x 300 mm tray 100 mm deep has a surface area of 2 x (400 x 100) + 2 x (300 x 100) + 400 x 300 = 260,000 mm², an opening area of 120,000 mm² and a draw ratio of about 2.17. To get a 1.5 mm wall, the starting sheet must be at least about 3.25 mm thick, not counting the extra thinning at the corners.
Industry design guides treat an average draw ratio of about 3:1 as the maximum, and parts are easiest when the depth does not exceed the width of the narrowest opening. You can enter your tray’s dimensions in the tool below for a quick estimate:
Which plastics can be used for thermoforming?
Most thermoplastics in sheet form can be thermoformed; the most common are PS (HIPS), PET and PETG, PVC, ABS, PP, HDPE, PC and acrylic (PMMA). Amorphous plastics such as PS, ABS and PETG are easiest; PP and HDPE are harder because of the narrow temperature window and high shrinkage.
For thin gauge food packaging, PS, PET and PP are the three most common materials. PET and PETG are clear and impact resistant, used for display boxes and medical packaging; according to Formech, PETG forms at a low temperature with a fast cycle and can be used in food applications. HIPS is cheap and easy to work, suited to simple trays and blister packs. ABS is rigid and impact resistant, often used for equipment housings and technical trays. PP is chemical resistant and barely absorbs moisture, but the sheet sags a lot when hot; Formech recommends PP copolymer rather than homopolymer for easier forming.
One difference buyers often forget is that some plastics absorb moisture. ABS and PC must be dried before forming, otherwise water vapour causes pitted blisters on the surface; Formech gives the example of a 3 mm PC sheet needing about 4 hours of drying. PS and PETG normally need no drying. When comparing quotes from two shops, ask clearly about the plastic type, the starting sheet thickness and the minimum wall thickness guaranteed at the corners.
What parameters matter for a thermoforming mould?
Four parameters decide whether the product can be released from the mould, has even walls and the right size: draft angle, corner radius, vacuum holes and shrinkage factor. All four should be settled with the shop from the drawing stage, because changing the mould afterward costs far more.
The draft angle must be larger on a male mould, because the plastic shrinks tightly onto the mould as it cools; on a female mould the plastic shrinks away from the wall so less is needed. Common design guides give a minimum of about 3 to 5 degrees for a male mould and 1 to 2 degrees for a female mould, and textured surfaces need extra. The corner radius should be at least the wall thickness so the plastic distributes evenly and stress concentration is reduced.
Vacuum holes must be small enough not to leave dents on the product; for more suction, increase the number of holes rather than the hole size. Shrinkage varies widely with the plastic: Formech lists PP at 1.5 to 2.2%, much higher than the amorphous group, so the mould has to be made larger than the product to suit the exact plastic that will be used. Moulds can be wood or epoxy for samples and small runs, or aluminium with cooling channels for mass production; this is why thermoforming moulds are usually much cheaper than a steel injection mould for a product of the same size.
When should you use thermoforming instead of injection moulding?
Choose thermoforming when the product is a tray, blister pack, lid, liner or large thin-walled part, with moderate volumes or frequently changing designs; choose injection moulding when you need even thick walls, ribs, threaded holes, load bearing and multi-tier stacking at large, stable volumes. The table below compares the two technologies on the criteria buyers often ask about.
| Criterion | Thermoforming | Injection moulding |
|---|---|---|
| Input material | Pre-extruded plastic sheet | Plastic pellets |
| Mould | Single-sided (male or female), wood, epoxy or aluminium | Two closed steel halves |
| Wall thickness | Uneven, thinnest at corners and edges | Even, controllable at each position |
| Two-sided detail, ribs, threaded holes | Limited, only the mould-contact face is sharp | Possible |
| Suitable volume | Small to medium (heavy gauge), very large (thin gauge) | Large, stable |
| Waste | Trimmed sheet edge, needs grinding and recycling | Little, mainly the sprue |
That is why load-bearing warehouse containers, such as solid-wall crates, plastic baskets and EU standard crates, are almost all injection moulded, as covered in detail in the separate article on injection moulding on the ICD blog. Thermoforming appears in logistics in a supporting role: divided trays placed inside a container to hold electronic components, small spare parts and bottles in place, with antistatic versions for circuit boards. The outer container still carries the load, while the inner tray is made to the shape of each part at low tooling cost. The outer container is usually chosen from standard industrial plastic containers or injection-moulded component trays.
In plastic container manufacturing, the decision between the two technologies usually comes down to volume and structural requirements. A heavy gauge part made in a few hundred to a few thousand pieces a year is in thermoforming’s favourable zone; once volumes rise to tens of thousands and tight tolerances are needed on both sides, a steel injection mould works out cheaper per product.
Frequently asked questions about thermoforming
What is a thermoformed plastic?
It is a plastic product made by softening a thermoplastic sheet by heating, then using vacuum, compressed air or a plug to press the sheet into a single-sided mould to form a 3D shape, followed by cooling and trimming. Common examples are trays, medicine blister packs, food containers, equipment housings and liners.
What steps does the thermoforming process include?
Clamp the sheet in a frame, heat it to forming temperature, press the sheet into the mould with vacuum or air pressure, hold on the mould to cool, release and trim. The excess edge is ground up to make sheet again.
How do vacuum forming and pressure forming differ?
Vacuum forming uses only atmospheric pressure, about 1 atm, so the mould and machine are cheap, suiting trays and blister packs. Pressure forming adds compressed air on the back of the sheet, usually up to about 50 psi, for sharp corners and a crisp surface close to injection moulding, but the mould must be more rigid.
Which plastics are commonly used in thermoforming?
The common ones are PS (HIPS), PET and PETG, PVC, ABS, PP, HDPE, PC and acrylic. PS, ABS and PETG are easiest to form; PP and HDPE are harder because of the narrow forming temperature window and high shrinkage.
How thick is thermoforming plastic sheet?
Thin sheet under 1.5 mm is used for packaging and fed from a roll; heavy sheet over 3 mm is used for large parts, fed one sheet at a time; the 1.5 to 3 mm range is medium gauge. The minimum starting sheet thickness is approximately the draw ratio multiplied by the desired wall thickness.
Is thermoforming expensive?
Tooling cost is much lower than injection moulding because only a single-sided mould in wood, epoxy or aluminium is needed. Heavy gauge work is especially economical at volumes of about 250 to 3,000 pieces a year; thin gauge work runs continuously on machines for very large volumes.
Why are thermoformed products thin at the corners?
Because the sheet is stretched to cover a surface larger than its starting area, and the part that touches the mould last, usually the corners and deep base, is stretched the most. Reduce this with larger corner radii, adequate draft, zone heating and a plug assist.
What parts does a thermoforming machine have?
A sheet clamp frame, a heater (usually infrared ceramic or quartz, divided into several zones), a raising and lowering mould table, a vacuum system or compressed air pressure box, cooling fans and a trimmer. Thin gauge machines feed plastic from a roll and run continuously; heavy gauge machines feed pre-cut single sheets.
What is a vacuum-formed plastic tray?
It is a tray made by vacuum forming from thin plastic sheet such as PET, PS, PVC or PP, with cavities shaped to the product to hold goods in place. This kind of tray is used as confectionery trays, electronic component trays and divided liners inside shipping containers.
Can thermoforming make load-bearing plastic containers?
It can make containers and large parts from heavy gauge sheet, but the walls are uneven and it is hard to form ribs and threaded holes as injection moulding does. Containers stacked many tiers high and bearing loads in warehouses are therefore usually injection moulded; thermoforming suits trays, lids and liners placed inside the container.
Contact ICD Vietnam
ICD Vietnam Industrial Manufacturing Co., Ltd
For advice on choosing plastic containers, component trays and divided layouts for your goods, please contact:
- Hotline: 0983 797 186 / 090 345 9186.
- Email: sales@icdvietnam.com.vn.
ICD Vietnam plastic containers carry a 12-month warranty under the warranty and repair policy published on the website.
References
- Wikipedia, Thermoforming: process, classification of thin sheet under 1.5 mm, medium sheet 1.5 - 3 mm, heavy sheet over 3 mm, heavy gauge volumes of 250 - 3,000 pieces a year.
- Formech, Vacuum Forming Guide: heating time by thickness, forming temperature, PP copolymer, PP shrinkage 1.5 - 2.2%, drying of moisture-absorbing plastics.
- Röhm, Thermoforming ACRYLITE acrylic sheet: air pressure in pressure forming, draft angle.
- Polyvantis, LEXAN Sheet: Processing, Forming and Fabricating Guide (2025): maximum draw ratio 3:1, corner radius, male and female mould draft angles.
- Society of Plastics Engineers, Thermoforming Division: technical resources on thermoforming.